Best Shearing Machine for Precision Metal Cutting and Fabrication
2026-10-21
Precision metal cutting often hinges on one critical decision: the right shearing machine. While many options promise clean edges and tight tolerances, only a handful truly deliver for demanding fabrication work. From reducing material waste to achieving repeatable accuracy, the difference between an average cut and a flawless one frequently comes down to machine design and build quality. At HUNSONE, we've spent years refining what a best-in-class shear should be. Here's what to look for before investing in your next precision cutting solution.
What Actually Determines a Clean, Square Cut Every Time
The clean, square cut starts long before the blade touches the wood. If the saw's arbor has even a slight wobble or the blade isn't seated flat against the flange, every cut will drift off square. A quick test with a dial indicator or a simple combination square against the blade teeth will reveal misalignment. Most of the time, the culprit is a dirty arbor flange or a blade that was dropped and now has a bent plate.
Fence alignment matters just as much. When the rip fence isn't parallel to the blade, the workpiece gets pinched between the fence and the blade's rising teeth, causing burn marks, rough edges, and a cut that's square at the front but angled at the back. Loosen the fence, run it along the miter slot, and lock it down while checking with a feeler gauge. Even a half-degree of toe-out can make a noticeable difference on longer boards.
Finally, don't ignore the blade itself and your feed rate. A dull or dirty blade forces you to push harder, which flexes the material and opens up the kerf. Use a blade with the right tooth count for the material, and feed steadily without stopping. Let the saw do the work, and you'll get that crisp, square edge without needing to sand or trim afterward.
Hydraulic vs. Mechanical: Matching Drive Type to Your Shop Floor
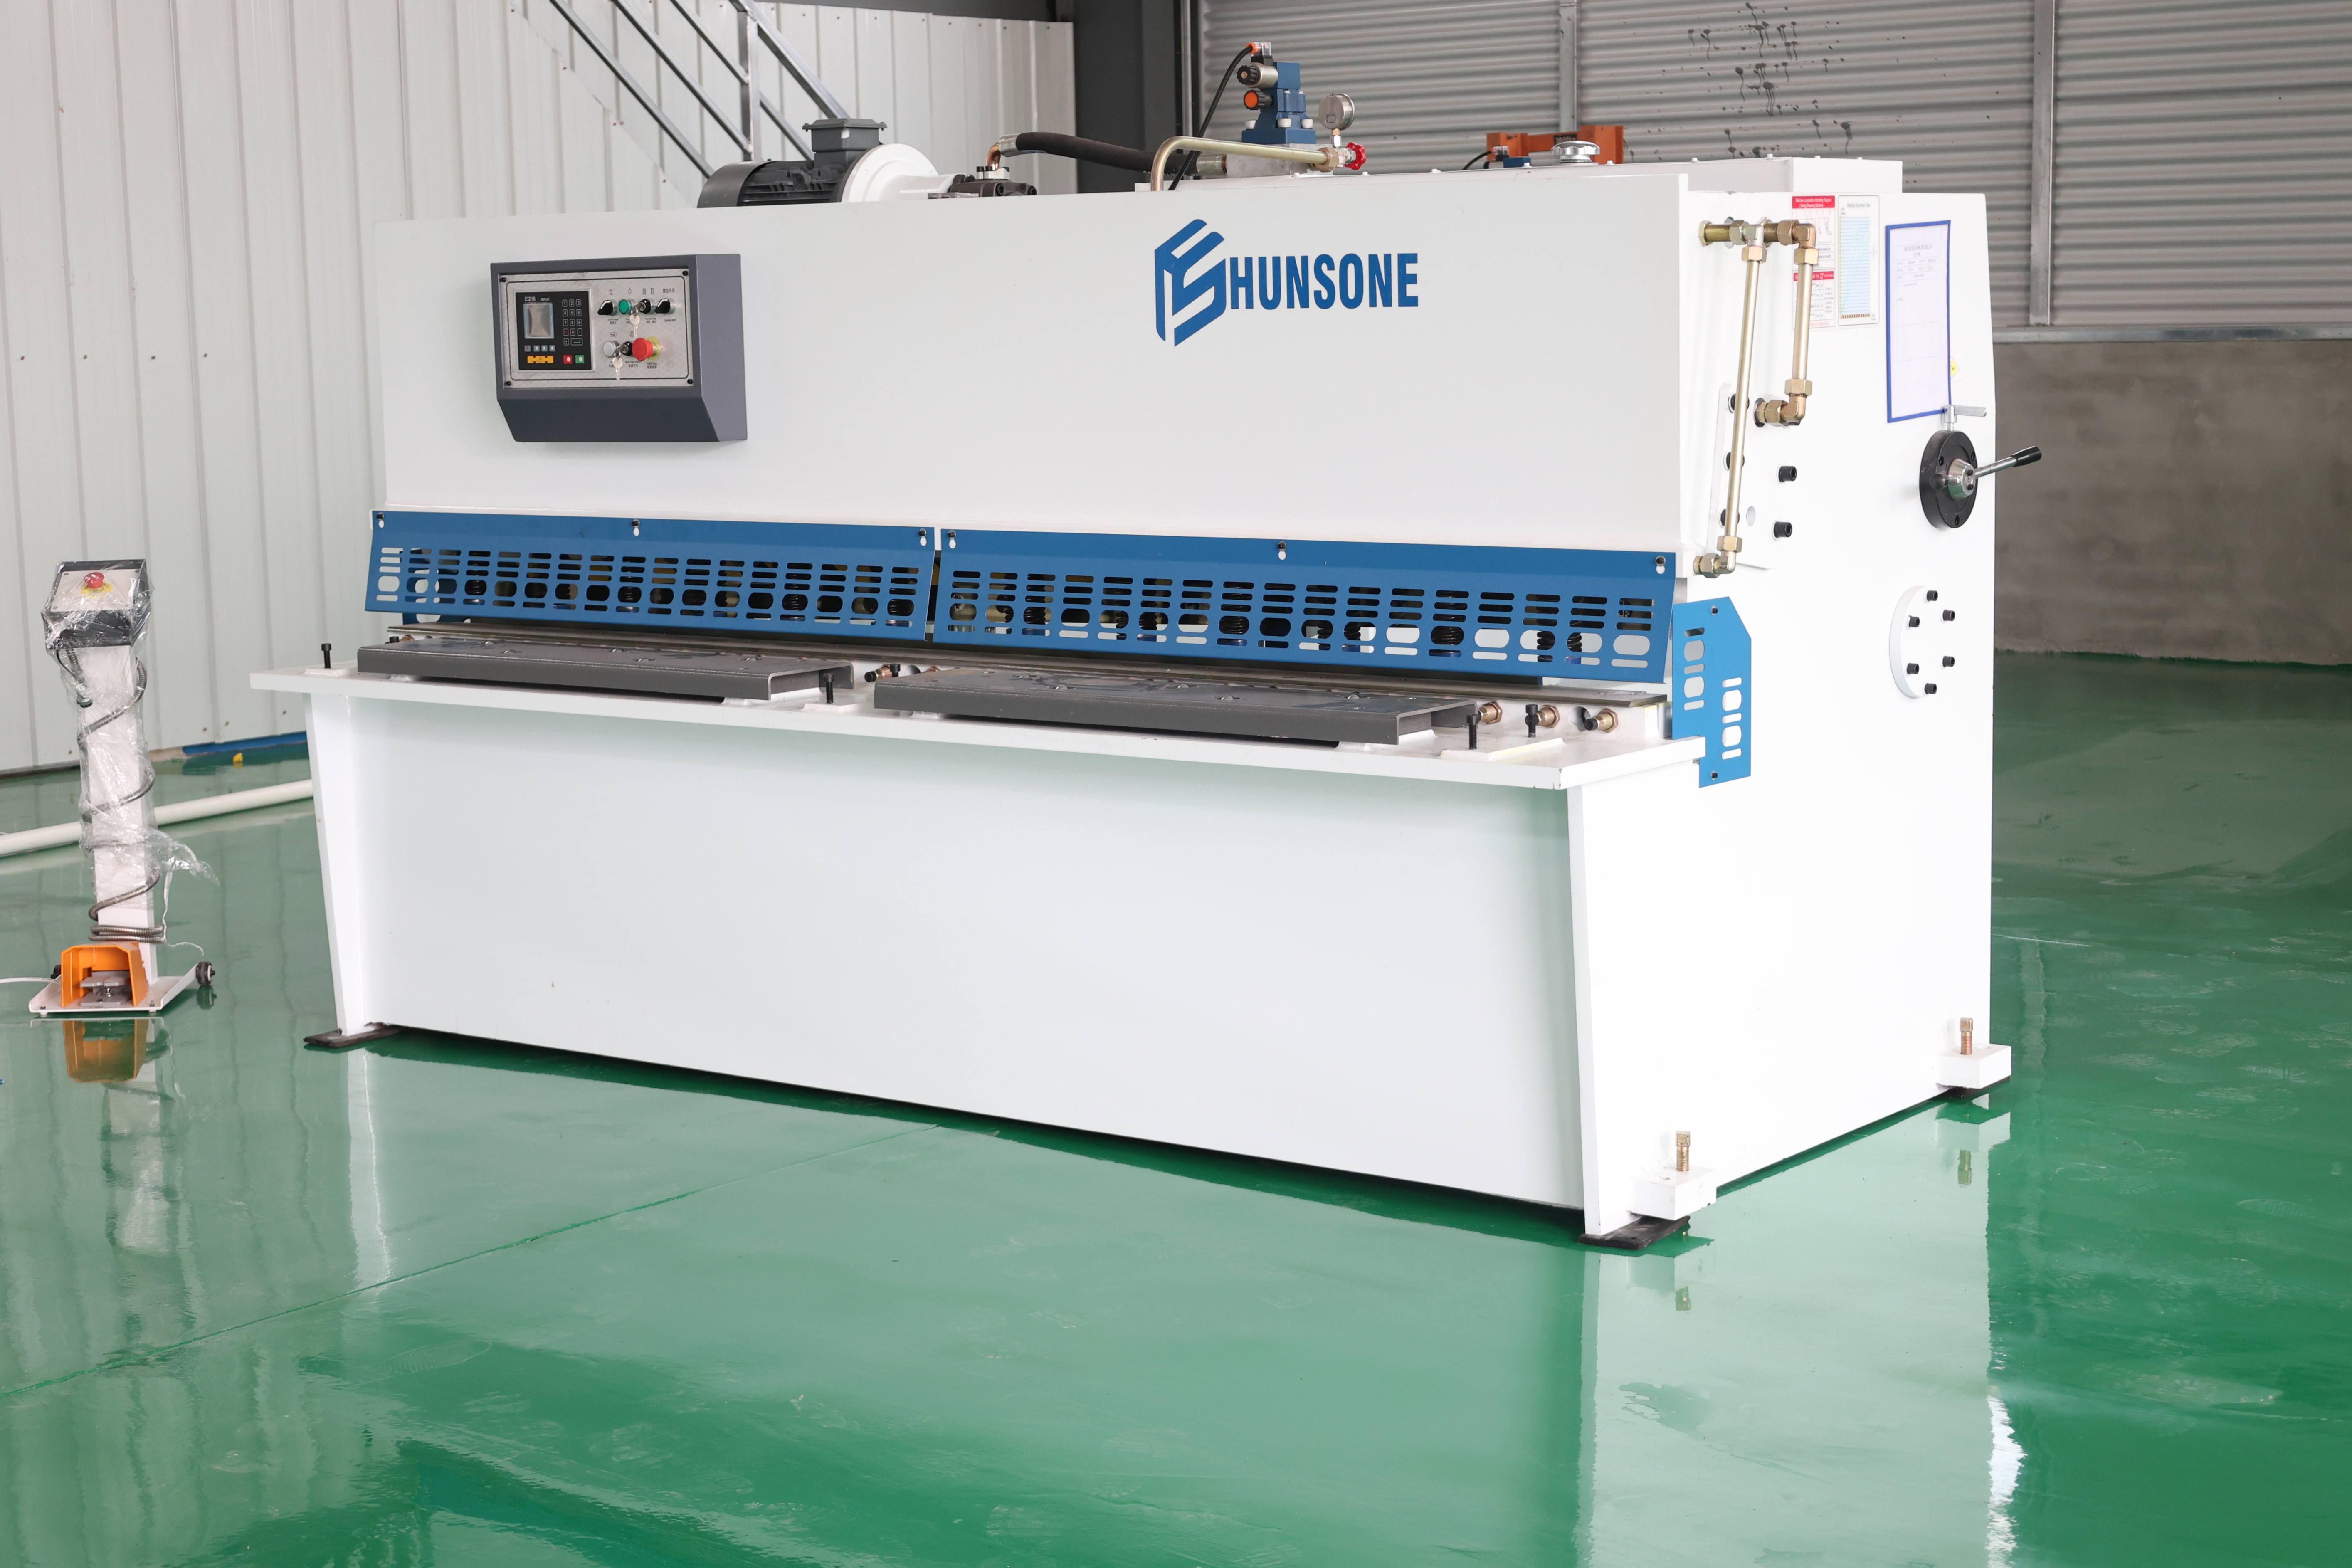
Hydraulic drives deliver smooth, variable power that shines when you need precise control or heavy lifting at a workstation. Mechanical drives, on the other hand, are straightforward and cheap to maintain, perfect for a fixed-pace conveyor line. Think about how often your floor area sees sudden loads or frequent starts and stops—that alone can push you one way or the other.
If your shop floor isn't perfectly level or has a slight slope, the rigid connection of a chain or gear drive tends to hold up better. Hydraulic systems don't like leaks, and oil on the floor is a slip hazard, so keep them in enclosed or easy-to-clean zones. Also, hydraulics build up heat when they cycle back and forth constantly, so check whether the floor area has enough ventilation to handle that.
In practice, the best match often comes down to who operates the equipment and what your maintenance crew already knows. Hydraulics need regular checks on oil levels and seals, while mechanical drives just want grease and tension adjustments. Lay out the floor plan, power source locations, and budget on one sheet, then run a small pilot in one corner before committing the whole line.
Why Blade Clearance and Rake Angle Matter More Than Horsepower
Most people look at engine specs first, but a machine's true ability to move material cleanly comes down to how the blade meets the surface. Blade clearance, the space between the cutting edge and the housing or bed, decides whether grass, snow, or soil gets sliced cleanly or torn and left behind. Too much clearance lets material slip through uncut; too little causes drag, heat, and premature wear. Rake angle then determines how aggressively the blade bites. A slight positive rake reduces load on the engine and leaves a cleaner finish, while a negative or blunt angle forces the motor to work harder for a ragged result.
Horsepower can mask sloppy geometry for a while, but it cannot fix it. A machine with less power but a properly set clearance and rake will often outperform a high-output unit with a dull or misaligned blade. That gap between edge and housing also affects how well air moves, which in turn controls discharge and clumping. Get both measurements right, and the blade shears instead of batters.
Field adjustments tell the story faster than any dyno sheet. If you are constantly clearing clogs, seeing uneven stubble, or hearing the engine labor under a light load, check clearance first. Then inspect the rake. Small changes of a few degrees or millimeters often deliver bigger gains than bolting on extra horsepower, because you are restoring the blade's intended cut rather than forcing it through with brute force.
Reading the Spec Sheet: Stroke Length, Throat Depth, and Backgauge
Stroke length tells you the maximum vertical travel of the press brake ram, but the number printed on the sheet rarely matches what you can actually use with tooling mounted. A machine rated for 200 mm of stroke might lose 30 mm or more once the upper punch, lower die, and any adapters are in place. Before quoting a deep box or tall flange, pull the tooling drawings and subtract the shut height from the open height—otherwise you may find the ram tops out before the part clears the die.
Throat depth sets the distance from the ram centerline to the frame casting, and it decides how far a pre-bent flange can reach into the machine. On a press brake with a 400 mm throat, you can form a 350 mm web with a modest flange, but that same web becomes a problem if the previous bend creates a tall return that hits the side housing. It is worth sketching the part mid-sequence, not just at the final angle, because the deepest reach often occurs on an intermediate bend.
Backgauge specs tend to hide the difference between repeatability and absolute positioning. A gauge that repeats to ±0.01 mm may still be off by 0.5 mm across the full X-axis if the linear guides or rack have wear. Check the spec sheet for the full stroke tolerance, not just the repeatability figure. Also note the number of axes and the physical finger size: a six-axis gauge sounds impressive, but if the fingers cannot drop below a narrow lower die, you will spend more time shimming than bending.
Common Setup Mistakes That Quietly Ruin Precision
The simplest way to lose precision is to trust a machine that hasn't been checked for squareness and tram. A tiny error in spindle alignment or a slightly tilted vise gets multiplied across long cuts. Most people chase the digital readout for answers, but the real culprit is often a fixture that shifts under load or a workpiece that wasn't stress-relieved. Take twenty minutes to indicate the table and the vise before you touch a cutter, and you'll stop fighting numbers that never seem to repeat.
Tool setup gets blamed less often but causes just as much trouble. A collet that hasn't been cleaned properly, a tool holder with a ding on the taper, or excessive stick-out can all introduce runout you won't notice until a hole comes out oval or a bore is tapered. Even a new carbide endmill will cut oversize if the shank isn't fully seated. Ignore the cheap dial indicator; it's the fastest way to find these problems before they become your final dimension.
Temperature and clamping order are the quiet killers. If you're holding tenths, a cold spindle and a warm part will never agree, no matter how carefully you probe. Clamping too tight or in the wrong sequence can bow a part by a few microns and release that error the moment the pressure comes off. Let the machine warm up, let the part normalize to the room, and tighten clamps in a cross pattern. Precision is less about expensive gear and more about refusing to let small setup details slide.
Maintenance Habits That Keep a Shearing Machine Within Tolerance for Years
Shearing machines stay accurate only when routine checks become second nature. Start by measuring blade clearance every forty hours of runtime — a slight widening here forces the metal to tear rather than cut cleanly, and tolerance drifts before anyone notices. Write down the readings on a laminated card taped near the control panel. That simple habit turns guesswork into a log you can trust.
Lubrication points often get ignored because they look fine from the outside. Yet dry ram guides or a neglected backgauge chain wear unevenly under load. Use a grease gun with a dedicated nozzle for each fitting, and wipe away old grease instead of layering new over hardened buildup. Operators who do this weekly can feel the difference in lever resistance — the machine almost tells you what it needs.
Hydraulic fluid tells a hidden story. Instead of waiting for a scheduled change, pull a small sample every month and rub it between your fingers. Gritty texture means seal wear; a burnt smell signals overheating. Replacing just the filter and topping off clean fluid when these signs appear costs far less than a cylinder rebuild later. Over years, these small attentive habits keep the shear cutting square without constant adjustment.
FAQ
Focus on the blade gap adjustment mechanism, the rigidity of the frame, and the quality of the backgauge system. A machine with a precise, easy-to-set blade clearance will handle different sheet thicknesses without excessive burr or twist, and a sturdy frame prevents deflection during the cut, which is often the hidden culprit behind angled or inconsistent edges.
Blade clearance needs to be tighter for harder, thinner materials like stainless steel—usually around 3-5% of material thickness—while mild steel can tolerate closer to 8-10%. If the gap is too wide, stainless tends to roll over or leave a heavy burr; too narrow and you risk chipping the blade. Many shops keep a quick-reference chart next to the machine rather than relying on memory.
Not always. Hydraulic machines offer smoother, adjustable stroke control and are generally safer for long production runs because they can hold the ram at any point. Mechanical shears are faster and cheaper upfront, but they deliver a fixed stroke, which can be overkill for thin sheet and harder to control for delicate cuts. If your work mixes 20-gauge stainless with 1/4-inch plate, hydraulic is usually worth the extra cost.
The two big ones are keeping the blade gap consistent across the full length and checking the backgauge squareness weekly. Wipe down and lightly oil the blades after every shift, especially if you cut galvanized or aluminum, which leave residue. Also, verify the hydraulic fluid level and filter if it's a hydraulic model—contaminated fluid causes erratic ram movement that shows up as wavy cuts.
Yes, but you need to adjust the rake angle and blade clearance differently than for steel. Aluminum and copper are softer and more prone to bending or dragging, so use a slightly larger blade gap (around 6-8% of thickness) and a lower rake angle to reduce twist. Also, avoid cutting abrasive materials like hardened alloys unless the blades are rated for it, because standard high-carbon steel blades dull quickly.
Look beyond the basic foot pedal guard. A transparent finger guard that covers the cutting zone, a two-hand or presence-sensing control to prevent accidental cycling, and a reliable blade gap with no pinch point at the back are key. Also, check if the machine has a manual blade gap setting that requires no reaching under the blade—this reduces the habit of unsafe shortcuts.
If your batches are under 20 pieces and sheet sizes change often, a manual backgauge with a digital readout is faster than people assume, and it's easier to repair. CNC backgauge makes sense when you repeat the same cut dimensions frequently or need angle and multi-stop positions without measuring each time. The real difference is setup time: CNC pays off around 50+ parts per week of the same profile.
Conclusion
A clean, square cut has less to do with raw tonnage than with how well the blade clearance and rake angle are dialed in for the material thickness. If those two settings drift even slightly, you get edge roll, burr, or a distorted blank no matter how powerful the machine is. On the shop floor, drive type also shapes everyday performance. Hydraulic shears offer consistent force through the stroke and handle varied stock without shock loading, while mechanical units can cycle faster but demand more attention to clutch and brake wear. Matching the drive to your typical batch sizes and material mix often matters more than chasing a higher horsepower number.
Reading beyond the headline capacity pays off too. Stroke length, throat depth, and backgauge travel determine whether a shear can handle full sheets, narrow strips, or repeat cuts without constant repositioning. Many precision problems start quietly during setup—clamped stock that slips, a backgauge squared against a worn reference edge, or blades installed with uneven clearance. Once cutting, the habits that keep a machine within tolerance are unglamorous but non-negotiable: checking blade gap with feeler gauges, cleaning chips from the table and guides, lubricating pivot points, and verifying backgauge squareness every few weeks. These routines, more than any brand badge, decide whether a shearing machine keeps producing accurate parts year after year.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/