Best MOCVD Susceptor Designs for Uniform Thin Film Deposition
2026-10-19
Uniform thin film deposition in MOCVD depends on a susceptor that delivers consistent temperature and gas distribution across every wafer. Yet all too often, subtle design flaws lead to thickness gradients, wasted runs, and lower yields. The most effective susceptor designs tackle this with tailored thermal profiles, precise pocket geometries, and high-purity SiC coatings that resist thermal shock and chemical attack. At Semicorex, these design priorities guide the development of susceptors for demanding LED, power electronics, and laser diode production. In the sections ahead, we break down what makes a susceptor design truly best-in-class for uniform thin film deposition.
Flattening Temperature Across the Wafer Without Overshooting the Center
Achieving a uniform temperature profile across a silicon wafer often turns into a balancing act. The center has less edge area for heat loss, so it naturally heats faster. If the control loop is tuned too aggressively to bring the edges up to target, the center can spike well past the setpoint before the system settles. A better approach is to use zone-based heating with independent edge and center control, where the center zone is deliberately driven with a softer response and the edge zone takes on more of the ramp duty. This keeps the midpoint temperature from running away while the edges catch up.
In practice, that means shaping the power profile instead of applying a single uniform setpoint across all lamps or resistive elements. Multi-point pyrometry or an array of thermocouples gives real-time feedback for each zone, allowing a model-predictive or cascaded PID scheme to weight the edge heaters more heavily during ramp-up. Once the wafer approaches soak temperature, the center zone can be brought back into balance with small, incremental adjustments. The result is a flat profile across the entire diameter, with no overshoot at the center and minimal risk of thermal stress or dopant diffusion drift.
Pocket Design: The Overlooked Lever for Uniform Precursor Flow
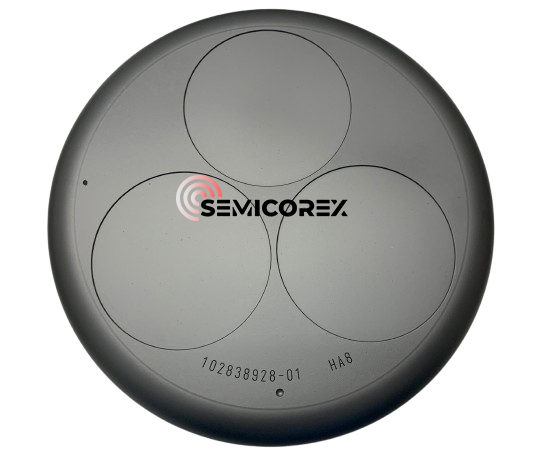
Most discussions around precursor delivery fixate on mass flow controllers, temperature ramps, or showerhead hole patterns. Yet the pocket’s geometry often dictates whether the gas reaches every wafer edge at the same moment. A shallow, sharply stepped pocket can force the incoming stream to accelerate near the inlet and stall in the far corners, producing that familiar center-to-edge thickness drift even when every other parameter looks stable.
Small changes—rounding the pocket floor, adjusting its depth relative to the wafer plane, or tapering the sidewall angle—shift how the precursor expands and mixes before it ever touches the substrate. These adjustments rarely show up on a process recipe sheet, but they routinely outweigh a few degrees of temperature trimming. When the pocket volume is properly matched to the inlet flow, the gas front arrives more evenly, reducing compensation loops and edge-defect workarounds.
It’s worth measuring what actually happens inside that cavity rather than assuming a nominally flat pocket is neutral. A slight asymmetry from machining tolerances or a misplaced exhaust slot can quietly create a preferred flow path. In many reactors, fixing the pocket contour yields a more uniform precursor flux than upgrading the gas panel or adding more sensors, simply because it addresses the first physical boundary the gas encounters.
Why Rotation Alone Won't Fix a Poorly Designed Susceptor
A rotating susceptor is often treated as a universal fix for temperature non-uniformity, but that assumption falls apart quickly when the design itself is flawed. If the susceptor has an uneven thickness profile or poorly machined pockets, rotation merely cycles the wafer through the same hot and cold zones. The wafer sees no real improvement; it just encounters the same defects at different angles.
The deeper issue is that rotation only averages out variations in the azimuthal direction. Radial gradients—from center to edge—remain fully intact. A poorly designed susceptor might have a thicker rim that retains more heat, or a central recess that distorts gas flow. Spinning the wafer cannot compensate for these structural asymmetries because every point on the wafer still traces the same radius and therefore spends exactly the same amount of time under the same flawed local conditions.
In some cases, rotation can even make things worse. If the susceptor warps at high temperature due to residual stress, a rotating wafer may rock slightly, changing the distance to the showerhead or heater and introducing new non-uniformities. The real fix is not to spin faster but to correct the susceptor geometry, material homogeneity, and support contact. Rotation is a finishing tool, not a repair for basic design errors.
Material Picks That Keep Susceptors Stable at 1,200°C and Beyond
Maintaining susceptor stability above 1,200°C demands more than just picking a high-melting-point metal. The real challenge lies in material choices that resist creep, oxidation, and thermal fatigue under repeated cycling. Molybdenum and tungsten often come to mind, but their susceptibility to embrittlement in oxidizing environments narrows their practical use unless paired with protective coatings or inert atmospheres. Graphite and silicon carbide offer alternative paths, each with distinct trade-offs: graphite excels in thermal shock resistance but requires careful handling to avoid particulate contamination, while silicon carbide provides excellent oxidation resistance yet may suffer from strength degradation if impurities creep in during high-temperature service.
For sustained operation at 1,200°C and beyond, alloyed molybdenum formulations—such as those with lanthanum or titanium-zirconium additions—help stabilize grain boundaries and reduce recrystallization, which is a common failure mode in pure moly. Another overlooked factor is the susceptor's emissivity and how it shifts with surface oxidation or coating wear. A material that starts with predictable RF coupling can drift out of spec as its surface chemistry evolves, leading to hot spots or uneven wafer heating. Selecting a material with a stable oxide layer, or applying a diffusion barrier coating like silicon carbide on graphite, keeps the susceptor's thermal response consistent over hundreds of cycles.
In practice, the best picks often combine a refractory core with a tailored surface treatment. For example, a graphite susceptor with a dense SiC coating can handle both the mechanical load and the oxidative environment, provided the coating's coefficient of thermal expansion is well matched to the substrate. Testing small coupons under actual process conditions—ramp rates, gas flows, and thermal gradients—remains the only reliable way to verify long-term stability. Cheap shortcuts, like using standard stainless steel or uncoated moly, may survive a few runs but will inevitably warp, crack, or contaminate the chamber well before the target lifespan is reached.
Coatings and Surface Finish: Stopping Deposition Where It Shouldn't Happen
Precision coating processes rarely fail because of the coating itself—they fail when material lands on surfaces that were never meant to be coated. Threads, sealing faces, electrical contacts, and bearing journals all suffer when overspray or vapor drift settles into a critical tolerance. The most reliable approach starts with engineering the surface finish to repel unwanted deposition long before masking tape ever touches the part.
A low-energy surface, achieved through passivation, electropolishing, or a thin fluoropolymer pre-treatment, changes how incoming coating droplets interact with the substrate. Instead of wetting and adhering, they bead up or slide away from high-precision zones. In vacuum deposition, controlled roughness matters just as much: a mirror-polished mask line creates a sharp transition, while a micro-roughened boundary encourages delamination and makes post-process cleanup far simpler.
The real skill lies in matching the surface finish to both the coating chemistry and the part’s end use. Hard chrome on hydraulic rods needs an entirely different masking philosophy than PVD titanium nitride on cutting tools. By treating unwanted deposition as a surface-energy problem rather than a masking-only problem, manufacturers can cut rework rates, extend tool life, and keep functional surfaces exactly where they belong.
Scaling Up Without Losing Flatness: Stress and Warpage in Large Trays
Large trays rarely fail from a single obvious cause. The flatness problems that appear at scale usually begin much earlier, in gate placement decisions and cooling channel layouts that looked harmless on a smaller mold. Once the part grows, even a modest difference in shrinkage between the center and the rim turns into visible twist or bow. What was once a cosmetic nuisance becomes a rejection issue because the tray no longer sits flush on automated handling equipment.
Residual stress in these parts is not evenly distributed. Thick ribs, bosses, and sudden wall transitions pull the surrounding material as it cools, creating local tension that can release days after molding. With large trays, that release often shows up as a corner lifting or a long edge curving inward. Waiting to measure flatness until the part is fully cooled and conditioned matters more than many tooling teams expect; a tray that measures flat at the press can be out of spec by the time it reaches the packing line.
Keeping a large tray flat is less about chasing a single magic parameter and more about balancing the entire thermal history. Slower, more uniform cooling through conformal channels or carefully positioned bubblers helps reduce the temperature gradients that drive warpage. Material choice also plays a quiet but decisive role: filled polypropylene and amorphous blends with lower, more predictable shrinkage often outperform unfilled resins in long, thin tray geometries. In practice, the most successful scale-ups treat flatness as a design target from the first mold flow simulation, not as a problem to be corrected after the first shots come out bowed.
FAQ
Graphite offers an unusual combination of high thermal conductivity, machinability, and resistance to thermal shock at typical MOCVD temperatures. It heats evenly under RF induction, which reduces localized hot spots that would otherwise create thickness gradients. While bare graphite reacts with ammonia or oxygen, a dense SiC coating preserves the thermal benefits while blocking surface erosion and outgassing, so the material remains practical for long production runs.
If the pocket is too shallow, the wafer edge sits above the surrounding surface and loses heat faster, producing a thick edge ring. If it is too deep, the recess traps gas and perturbs the boundary layer over the wafer center, causing non-uniform precursor delivery. A depth close to wafer thickness keeps the top surface nearly coplanar with the susceptor, which stabilizes both temperature and flow fields across the wafer.
Tighter spacing increases throughput but makes each pocket compete for heat and precursor gas. That competition often shows up as crescent-shaped thickness patterns on wafers near the gas inlet or exhaust. Wider spacing gives every wafer a more isolated boundary layer and reduces thermal shadowing, at the cost of fewer wafers per run. High-uniformity processes usually settle on a spacing that keeps edge depletion zones from overlapping.
A rotating inner plate decouples wafer rotation from the outer gas distribution ring. That means the wafers can spin fast enough to average out local flow irregularities, while the outer part stays fixed and maintains a stable thermal boundary. It also simplifies replacement because the inner plate, which sees the most wear, can be swapped without replacing the whole heater assembly.
Yes, because they redirect spent gases away from the wafer surface before recirculation cells can form. A shallow channel near the pocket edge can break up a vortex that would otherwise deplete the precursor over one side of the wafer. The key is keeping the channel dimensions small relative to the pocket diameter; anything too deep disrupts the thermal mass locally and creates a cold stripe.
Rotation is excellent at averaging azimuthal variation, but it cannot correct a radial temperature drop from center to edge. Multi-zone heating lets the edge zone run hotter than the center to offset those losses. This matters most in large-diameter susceptors or high-pressure processes, where thermal boundary layer thickness changes radially and alters the precursor cracking rate.
Look for visible pinholes in the SiC coating, a change in surface roughness near the pocket edges, or a slow upward drift in sheet resistance non-uniformity across test wafers. If particle counts rise after cleaning cycles, the base graphite is likely exposed and reacting with process gases. At that point, aggressive cleaning only accelerates degradation, so recoating or replacing the plate is the safer route.
Conclusion
Getting the temperature right across a wafer is rarely solved by heater tuning alone. The center captures heat faster than the edge, and pushing extra power to the outer zone often overshoots, leaving a hot ring instead of a flat profile. A more reliable fix is to embed the compensation in the susceptor itself—varying pocket depth, adding thermal breaks, or using a thicker rim to slow edge losses. Pocket design shapes more than temperature. A shallow pocket with tight side clearance keeps the wafer nearly flush with the tray surface, so the precursor stream stays attached and deposits evenly. Deep or loose pockets create small recirculation zones where gas stalls, forms particles, and drives thickness non-uniformity. Wafer rotation can smear some of these defects, but it cannot correct a broken flow field.
At 1,200°C and higher, the substrate choice separates designs that last from those that drift. Graphite with a dense CVD SiC coating remains the standard because it resists oxidation and outgassing, but the coating's thickness and grain structure matter—too thin and the graphite leaks, too thick and thermal mismatch causes microcracks. That coating also keeps deposition from happening where it should not, especially on the pocket rims and backside, which would otherwise shift wafer seating and alter the gas gap. Scaling to large multi-wafer trays adds another layer of difficulty. Thermal stress across a 300 mm or larger plate can bow the surface by tens of microns, changing local pocket depth and flow resistance. Backside ribs, tailored thickness profiles, and stress-relief cuts help hold flatness from the center to the edge. Without that attention, a design that works beautifully on a single wafer falls apart when the tray grows.
Contact Us
Contact Person: Svenja Wei
Email: [email protected]
Tel/WhatsApp: +8613567891907
Website: https://www.semicorex.com